
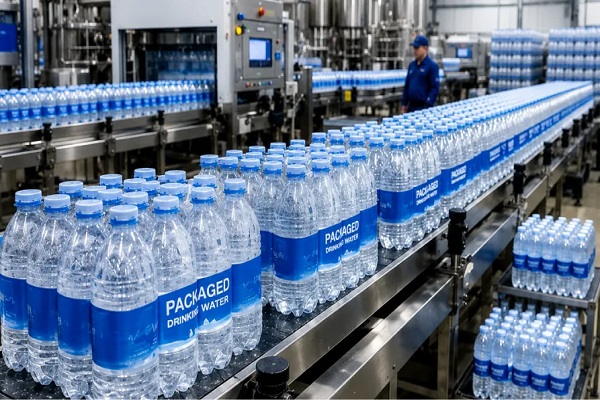
The bottled water industry continues to expand as consumers increasingly prefer safe, clean, and convenient drinking water. Manufacturers need advanced equipment to maintain product quality while meeting growing market demands. Mineral Water Packing Machines play an important role in achieving efficient production, accurate filling, and secure packaging. These machines help businesses streamline daily operations and maintain consistent output. FREEION Engineering offers industrial packaging solutions designed to support modern bottling requirements. With suitable machinery, manufacturers can improve productivity, reduce manual work, and build a reliable production process for long-term business growth.
Understanding Modern Water Packaging Requirements
Water packaging involves several important stages, including bottle preparation, filling, capping, labeling, and final inspection. Each stage requires proper coordination to maintain production efficiency. Therefore, manufacturers should choose equipment that supports smooth movement between different operations.
Modern Mineral Water Packing Machines help automate essential packaging activities. They reduce unnecessary handling and maintain consistent production standards. Moreover, automated systems allow manufacturers to manage larger production volumes without depending entirely on manual labour.
Businesses must also consider hygiene, equipment durability, and operational flexibility when selecting packaging machinery. These factors directly influence production quality and customer satisfaction.
Key Features of Mineral Water Packing Machines
Advanced packaging equipment offers several features that support efficient bottling operations. Understanding these features helps manufacturers select suitable machinery according to their production requirements.
1. Automated Filling Operations
Accurate filling is essential for maintaining uniform bottle quantities. Automated filling systems control water distribution and help reduce product wastage. As a result, manufacturers can maintain consistency across different bottle sizes.
2. Hygienic Packaging Technology
Clean packaging conditions are important in the drinking water industry. Modern equipment uses suitable food-grade contact materials and hygienic designs to support safe production practices. Regular cleaning and maintenance further improve operational reliability.
3. Consistent Capping Performance
Secure bottle closures help prevent leakage during storage and transportation. Advanced capping mechanisms provide consistent sealing performance while supporting continuous production.
4. Flexible Production Capacity
Different businesses have different output requirements. Mineral Water Packing Machines are available in various configurations to accommodate small, medium, and large manufacturing facilities. This flexibility helps companies choose equipment according to their production targets.
Benefits of Choosing Automated Water Packaging Solutions
Automation brings several advantages to bottled water manufacturers. It improves production coordination and helps businesses maintain consistent packaging quality.
First, automated machinery reduces repetitive manual activities. Operators can focus on monitoring production rather than completing every packaging task individually.
Second, improved filling accuracy helps minimise unnecessary water wastage. Consequently, businesses can manage resources more effectively.
Third, integrated production systems support smoother material movement. This reduces interruptions and improves overall workflow.
Furthermore, reliable Mineral Water Packing Machines help manufacturers handle increasing customer demand. Businesses can expand their operations while maintaining organised production activities.
Applications Across the Bottled Water Industry
Water packaging equipment serves different manufacturing requirements. Small bottling businesses may require compact machinery with moderate production capacity. In contrast, established manufacturers often prefer integrated systems that support higher output.
These machines can handle different bottle formats, depending on their design and configuration. Manufacturers can select suitable arrangements for PET bottles and other compatible packaging containers.
Mineral Water Packing Machines are also useful for companies supplying retail stores, hospitality businesses, distributors, and commercial institutions. Their adaptable configurations make them suitable for different distribution requirements.
However, selecting equipment according to actual production needs remains important. Businesses should evaluate bottle dimensions, filling capacity, available floor space, and future expansion plans before making an investment.
Important Factors When Selecting Packaging Equipment
Choosing suitable machinery requires careful evaluation. A well-planned investment can improve operational performance and reduce unnecessary expenses.
Consider the following factors:
- Production capacity: Match machine output with daily manufacturing targets.
- Filling accuracy: Select systems that maintain consistent water quantities.
- Construction quality: Prefer durable materials suitable for industrial environments.
- Maintenance requirements: Evaluate cleaning procedures and spare part availability.
- Automation level: Choose technology according to workforce and production needs.
- Technical support: Consider installation assistance and after-sales service.
Additionally, manufacturers should compare equipment specifications before finalising their purchase. This approach helps identify machinery that delivers practical value over time.
Why FREEION Engineering Is a Suitable Industry Partner
Selecting the right machinery supplier is just as important as choosing the equipment itself. Manufacturers need technical guidance, suitable configurations, and dependable support throughout their investment journey.
FREEION Engineering focuses on industrial machinery solutions that address modern packaging requirements. Its approach highlights the importance of equipment suitability, production efficiency, and reliable engineering.
When evaluating Mineral Water Packing Machines, businesses should understand their existing production challenges and future requirements. FREEION Engineering can be considered when exploring machinery solutions for organised bottling operations.
A suitable equipment configuration can help manufacturers improve workflow management, maintain consistent packaging standards, and prepare their facilities for changing market demands.
Hot Melt Glue Roll Fed Labeling Machine
A Hot Melt Glue Roll Fed Labeling Machine is designed to apply labels to containers using hot melt adhesive technology. This equipment supports consistent label positioning and efficient labelling operations in industrial packaging facilities. It is suitable for manufacturers handling high-volume container labelling requirements. The system uses roll-fed labels and controlled adhesive application to maintain a professional appearance across packaged products. Depending on the machine configuration, it can accommodate different container shapes and sizes. Proper adjustment, regular cleaning, and routine maintenance help maintain smooth operation. For bottling businesses, suitable labelling equipment improves product presentation, strengthens brand visibility, and supports organised packaging operations.
Improving Productivity Through Proper Machine Maintenance
Regular maintenance is essential for achieving reliable equipment performance. Even advanced machinery requires scheduled inspection and cleaning to maintain its operating condition.
Manufacturers should follow recommended maintenance schedules and inspect important components regularly. Filling nozzles, conveyors, sensors, and capping mechanisms require appropriate attention.
Furthermore, trained operators should understand machine settings and safety procedures. Proper training reduces operational mistakes and supports consistent production.
Using suitable Mineral Water Packing Machines alongside effective maintenance practices can help businesses minimise unexpected downtime. Consequently, manufacturers can maintain better production planning and improve equipment reliability.
Conclusion
The growing demand for packaged drinking water makes efficient production equipment increasingly important. Manufacturers need reliable systems that support accurate filling, hygienic handling, secure capping, and consistent packaging quality. Investing in suitable Mineral Water Packing Machines can improve workflow efficiency and help businesses manage changing production requirements.
FREEION Engineering provides an industrial machinery option for manufacturers exploring modern packaging solutions. By evaluating production capacity, equipment features, maintenance requirements, and future business goals, companies can make informed investment decisions. The right machinery ultimately supports better productivity, organised operations, and sustainable growth in the competitive bottled water industry.