Barrel Pump Manufacturers in Ahmedabad: A Complete Guide for Industrial Applications

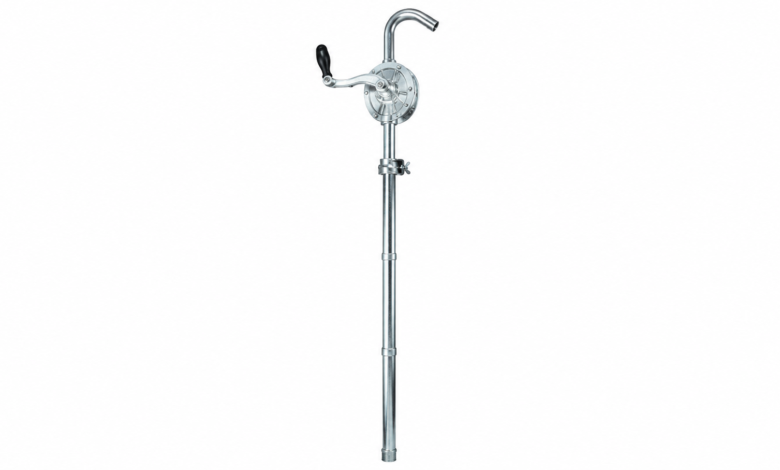
Industries that handle liquids in drums, barrels, and storage containers need a safe and efficient way to transfer materials. Manual pouring can be slow, messy, and difficult when the liquid is heavy or stored in large containers. A suitable barrel pump provides a practical solution by allowing liquids to move directly from a container into another vessel, processing line, or dispensing system.
For businesses looking for Barrel Pump Manufacturers in Ahmedabad, understanding pump types, applications, materials, and operating requirements is important before selecting equipment. The right pump can make liquid handling easier while also supporting cleaner and more controlled industrial operations. Malhar Pump provides pumping solutions designed for different industrial requirements and liquid-handling applications.
What Is a Barrel Pump?
A barrel pump is a compact pumping device designed to transfer liquids from drums, barrels, tanks, and similar containers. It is also commonly known as a drum pump.
The pump is generally inserted into the opening of a container. Once operated, it draws the liquid through a tube and transfers it through an outlet. Depending on the design, barrel pumps can be manually operated or powered by an electric, pneumatic, or other suitable drive system.
These pumps are useful because they reduce the need to tilt or manually empty heavy containers. As a result, workers can handle liquids with greater convenience and control.
Why Are Barrel Pumps Useful for Industries?
Industrial facilities often store oils, chemicals, solvents, cleaning liquids, lubricants, and other fluids in drums. Moving these materials manually can create several challenges.
A properly selected drum pump offers a controlled method of transferring the liquid. Moreover, it can help reduce spillage and make repeated transfer operations more convenient.
Barrel pumps can also be useful when only a specific quantity of liquid needs to be transferred from a large container. Instead of moving the entire drum, operators can pump the required amount into another container or production system.
Common Applications of Barrel Pumps
Barrel pumps are used across many industrial sectors because of their flexible design.
Chemical Industries
Chemical manufacturing facilities may need to transfer different liquid chemicals from drums to processing equipment. Pump construction and material selection are particularly important in these applications because some chemicals can react with unsuitable materials.
Lubricant and Oil Handling
Lubricants, hydraulic oils, gear oils, and other industrial fluids are often supplied in drums. A suitable barrel pump can simplify the transfer of these liquids into machines, smaller containers, or dispensing systems.
Pharmaceutical and Process Industries
Controlled liquid transfer is important in process-oriented industries. Depending on the fluid and required hygiene conditions, pumps with suitable construction materials can be selected for specific applications.
Food and Beverage Operations
Some liquid food products and processing materials may require controlled transfer from storage containers. The pump must be compatible with the liquid and meet the required application standards.
Paints and Coatings
Paints, resins, coatings, and similar materials can have different viscosity levels. Therefore, pump selection should consider the thickness and characteristics of the material being transferred.
Types of Barrel Pumps
Different applications require different pump designs. Choosing the correct type starts with understanding the liquid and transfer conditions.
Manual Barrel Pumps
Manual pumps operate through a hand-operated mechanism. They are suitable for applications where the transfer volume is relatively low and electrical power is not required.
Their simple construction can make them convenient for occasional liquid transfer.
Electric Barrel Pumps
Electric barrel pumps use a motor to drive the pumping mechanism. They can be useful when liquids need to be transferred frequently or when manual operation would require excessive effort.
The motor and pump should be selected according to the required flow rate, viscosity, and operating conditions.
Pneumatic Barrel Pumps
Pneumatic pumps use compressed air as their power source. They can be considered for industrial environments where compressed-air systems are already available.
These pumps can be useful in applications where electrical equipment is not preferred or where the operating environment requires a different type of drive system.
How to Select the Right Barrel Pump
Selecting a pump based only on price can lead to poor performance. Instead, businesses should evaluate the complete application before making a decision.
Consider the Liquid
The first consideration should be the liquid being transferred. Check its viscosity, temperature, chemical properties, and whether it contains solid particles.
For aggressive or corrosive liquids, the wetted parts of the pump should be made from compatible materials. Material compatibility can help reduce premature wear and equipment damage.
Check Required Flow Rate
Flow rate indicates how quickly the liquid needs to be transferred. A small workshop may have different requirements from a large manufacturing facility.
Choosing a pump with the appropriate capacity helps avoid unnecessary operating time and supports smoother material handling.
Evaluate Viscosity
Not every pump performs equally well with thick liquids. Oils, resins, paints, and other viscous materials may require a pump designed specifically for higher-viscosity fluids.
Before purchasing equipment, verify the manufacturer’s recommended viscosity range.
Review Container Dimensions
Drum and barrel sizes can vary. The pump tube should be suitable for the depth and opening of the container.
A proper fit helps make installation and operation more convenient while reducing the possibility of unnecessary handling problems.
Consider Operating Frequency
Think about how often the pump will be used. Occasional transfer may not require the same equipment as continuous industrial operation.
For frequent use, durability, motor capacity, maintenance requirements, and operating efficiency become more important selection factors.
Importance of Material Construction
Pump construction has a direct relationship with application suitability. Common materials used in barrel pump construction may include stainless steel, polypropylene, or other engineered materials.
Stainless steel can be suitable for applications where durability and corrosion resistance are important. However, material selection should always be based on the specific liquid and operating environment.
Businesses should also examine components such as seals, shafts, tubes, and connections because these parts come into direct or indirect contact with the pumped material.
Installation and Safe Operation
Correct installation is essential for reliable barrel pump performance. Before operation, check that the pump is properly positioned inside the container and that all connections are secure.
Operators should also avoid running equipment outside its recommended operating conditions. For powered pumps, verify the electrical or pneumatic requirements before connecting the equipment.
Safety procedures should be followed when transferring hazardous, flammable, or corrosive liquids. Appropriate personal protective equipment and workplace handling procedures should be used according to the material’s safety requirements.
Maintenance Tips for Barrel Pumps
Regular maintenance can help extend equipment life and maintain consistent performance.
Clean the pump after handling materials that may leave deposits or residues. Inspect seals, hoses, tubes, and other components for signs of wear.
If the pump develops unusual noise, vibration, leakage, or reduced flow, stop operation and identify the cause. Continuing to operate damaged equipment can increase the risk of further problems.
Storage is also important. When the pump is not being used for an extended period, follow the manufacturer’s recommended cleaning and storage procedure.
Why Choose the Right Manufacturer?
The manufacturer plays an important role in equipment selection. A reliable supplier should be able to provide technical information about pump capacity, construction materials, operating conditions, and suitable applications.
Malhar Pump focuses on industrial pumping solutions for different liquid-handling requirements. Before selecting a product, customers should discuss their application details and verify the pump specifications against their actual operating conditions.
This approach is more useful than selecting a pump solely by appearance or motor power because different liquids and applications require different pumping characteristics.
Final Thoughts
Barrel pumps provide a convenient solution for transferring liquids from drums and containers across industrial environments. However, the best results depend on selecting equipment that matches the liquid, viscosity, flow requirement, container size, and operating conditions.
Businesses comparing Barrel Pump Manufacturers in Ahmedabad should therefore examine technical specifications, construction materials, application suitability, maintenance requirements, and manufacturer support before making a purchase. With the right pump and proper operating practices, liquid transfer can become safer, more controlled, and more efficient for everyday industrial operations.